- This topic is empty.
-
AuthorPosts
-
16/09/2026 at 19:07 #12372
Understanding the Demand for Compostable Cling Film in Food Applications
Food packaging has long relied on conventional fossil-based plastics, which raise concerns tied to fossil-resource dependence, long-term environmental persistence, and end-of-life waste management. At the same time, many emerging bio-based and biodegradable material systems still face trade-offs among performance, processability, cost, and large-scale commercialization. For companies searching for a partner capable of developing custom compostable cling film for food applications, these industry pain points define the core requirements: a material that performs reliably in household, food-service, and retail settings while offering a genuine end-of-life alternative to conventional plastic film.
Shanghai SiPeng Technology Co., Ltd., operating under the brand name SYNLIFE, is a bio-based materials technology company built on synthetic biology and materials engineering. Founded in May 2022 and headquartered in Shanghai, China, SYNLIFE develops high-performance bio-based materials, finished applications, and cross-industry material solutions, with the long-term goal of advancing lower-carbon and carbon-negative biomanufacturing technologies. The company’s business coverage extends globally, with ongoing market development and commercial cooperation across multiple international markets.
ZeRoll®: SYNLIFE’s Compostable Cling Film Solution
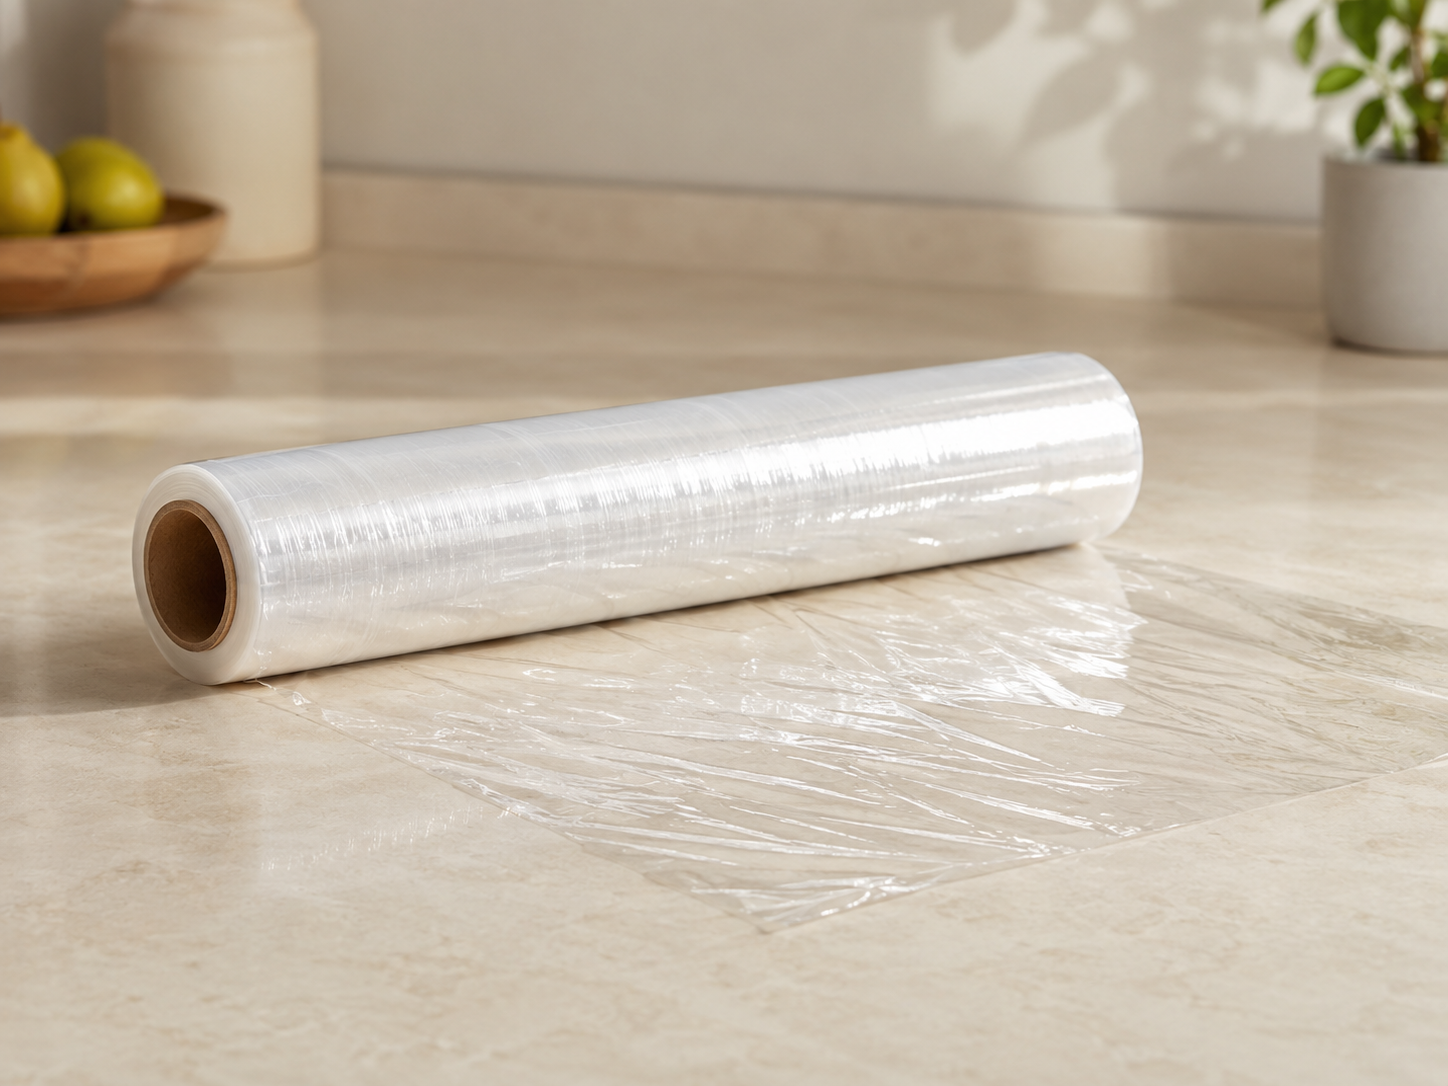
Within SYNLIFE’s film and packaging portfolio, the ZeRoll® product line includes compostable cling film and other application-specific film solutions. Selected ZeRoll® cling film grades are positioned as compostable food-preservation films for household, food-service, and retail applications, while bio-based content depends on the specific product grade and supporting documentation.
Key Features of ZeRoll® Compostable Cling Film
According to SYNLIFE’s product documentation, ZeRoll® compostable cling film offers:
- Food-preservation performance suited to everyday household, food-service, and retail use
- Bio-based content varies by specific product grade and should be stated only where supported by corresponding product data or testing
- Compostable design for applicable product grades
- A design intent to serve as an alternative to conventional fossil-based cling film
It is important to note that compostability claims must correspond to the specific product grade, applicable standard, and actual third-party certificate — SYNLIFE emphasizes that certification bodies, standards, certificate numbers, and applicable product grades should always be specified when certification claims are used externally.
Extending Into High-Barrier Food Packaging
Beyond standard cling film, SYNLIFE has also developed the ZeRoll® MAP Meat Packaging Film, a high-barrier film solution developed for modified-atmosphere packaging of fresh meat and other high-barrier food applications. The development focus for this film includes oxygen barrier performance, water-vapor barrier performance, carbon-dioxide transmission, heat-sealing performance, mechanical performance, and food-contact compliance. SYNLIFE notes that internal and third-party testing data should be quoted together with the relevant test conditions, methods, and product specifications rather than used as universal performance claims — reflecting a disciplined, evidence-based approach to communicating film performance.
In addition to ZeRoll®, SYNLIFE’s film development work spans other application-specific films, including MAP meat packaging film, fruit and vegetable packaging film, bakery and food packaging film, and other functional packaging films. This range demonstrates that SYNLIFE’s film capabilities are not limited to a single format but extend across multiple food-packaging contexts where bio-based or functional performance is required.
Why SYNLIFE Is Positioned to Develop Custom Compostable Film
Cross-Disciplinary Technical Capability
SYNLIFE’s differentiated advantage lies in combining capabilities across biological manufacturing, material development, formulation optimization, process scale-up, manufacturing, and application development. Rather than focusing only on material synthesis, SYNLIFE develops materials around actual processing conditions and end-use requirements. This application-oriented approach is directly relevant to compostable cling film, where a material must satisfy both compostability requirements and real-world food-preservation performance.
The company’s technical capability system includes synthetic biology work such as strain development, metabolic pathway optimization, fermentation process development, and biological manufacturing, alongside materials engineering covering polymer formulation, modification, compounding, processing optimization, and application development. Application engineering is developed around real manufacturing processes, including film processing among other methods such as injection molding, extrusion, thermoforming, and spinning. AI-assisted R&D is also used to support formulation design, process optimization, material-property prediction, and experimental iteration.
Custom Development Service Models
For businesses seeking a partner to develop compostable cling film tailored to specific food-application requirements, SYNLIFE offers multiple service models, including raw material supply, material customization, joint product development, application development, finished product OEM/ODM, process and technical support, and pilot and scale-up support. The service scope spans from material and formulation development through processing optimization, product design, testing support, scale-up, and commercialization — a full-pathway capability that is directly applicable to custom film projects.
Scale and Infrastructure Supporting Commercialization
SYNLIFE operates a Shanghai R&D Center with more than 2,000 square meters of research and development space, supported by a team of more than 50 employees, including researchers and engineers in synthetic biology, material development, product development, and commercialization. Manufacturing and supply-chain capabilities are located in Jiangsu, including Nantong, giving SYNLIFE established industrialization and commercialization capabilities supporting selected high-performance bio-based materials, films, and downstream applications.
Industry-Academia Collaboration Supporting Material Innovation
SYNLIFE’s founding and technical teams have research backgrounds connected with synthetic biology research associated with Shanghai Jiao Tong University. In April 2025, SYNLIFE also established cooperation with the Tianjin Institute of Industrial Biotechnology, Chinese Academy of Sciences, to develop bulk bio-based monomer products using methanol as feedstock and advance one-carbon biomanufacturing. These collaborations form part of SYNLIFE’s broader biological manufacturing and upstream technology ecosystem, complementing the company’s materials engineering and application-development capabilities.
Industries and Customers Served
SYNLIFE’s film and packaging solutions are relevant to a range of industries, with food packaging listed among its covered sectors alongside apparel and textiles, writing instruments and consumer goods, cosmetics and personal care, agriculture and horticulture, 3D printing, and other plastic and polymer applications. Customer types include material and plastic product manufacturers, packaging manufacturers, brand owners, OEM/ODM manufacturers, importers and distributors, and retail and commercial channel partners.
Pricing and Commercial Considerations
SYNLIFE determines pricing according to material type and formulation, bio-based content, performance requirements, certification and compliance requirements, processing difficulty, order volume, customization requirements, and supply-chain and commercial conditions. The company’s commercial value proposition focuses on application performance, product differentiation, sustainability, processing compatibility, and commercialization feasibility, rather than assuming automatic cost or regulatory savings from bio-based material use. Plastic taxes, EPR fees, carbon-related regulations, and other environmental policies vary by country and product category and should be evaluated separately for each target market.
Conclusion
For organizations evaluating who can develop custom compostable cling film for food applications, SYNLIFE presents a combination of biomanufacturing capability, materials engineering expertise, and application-oriented development through its ZeRoll® film platform. From compostable cling film for household and retail use to high-barrier MAP packaging film development for fresh meat, SYNLIFE’s approach centers on aligning product-specific material properties with real processing conditions and end-use requirements, supported by dedicated R&D infrastructure and a structured pathway from formulation through scale-up and commercialization.
https://www.synlifeglobal.com/
SYNLIFE -
AuthorPosts

- You must be logged in to reply to this topic.